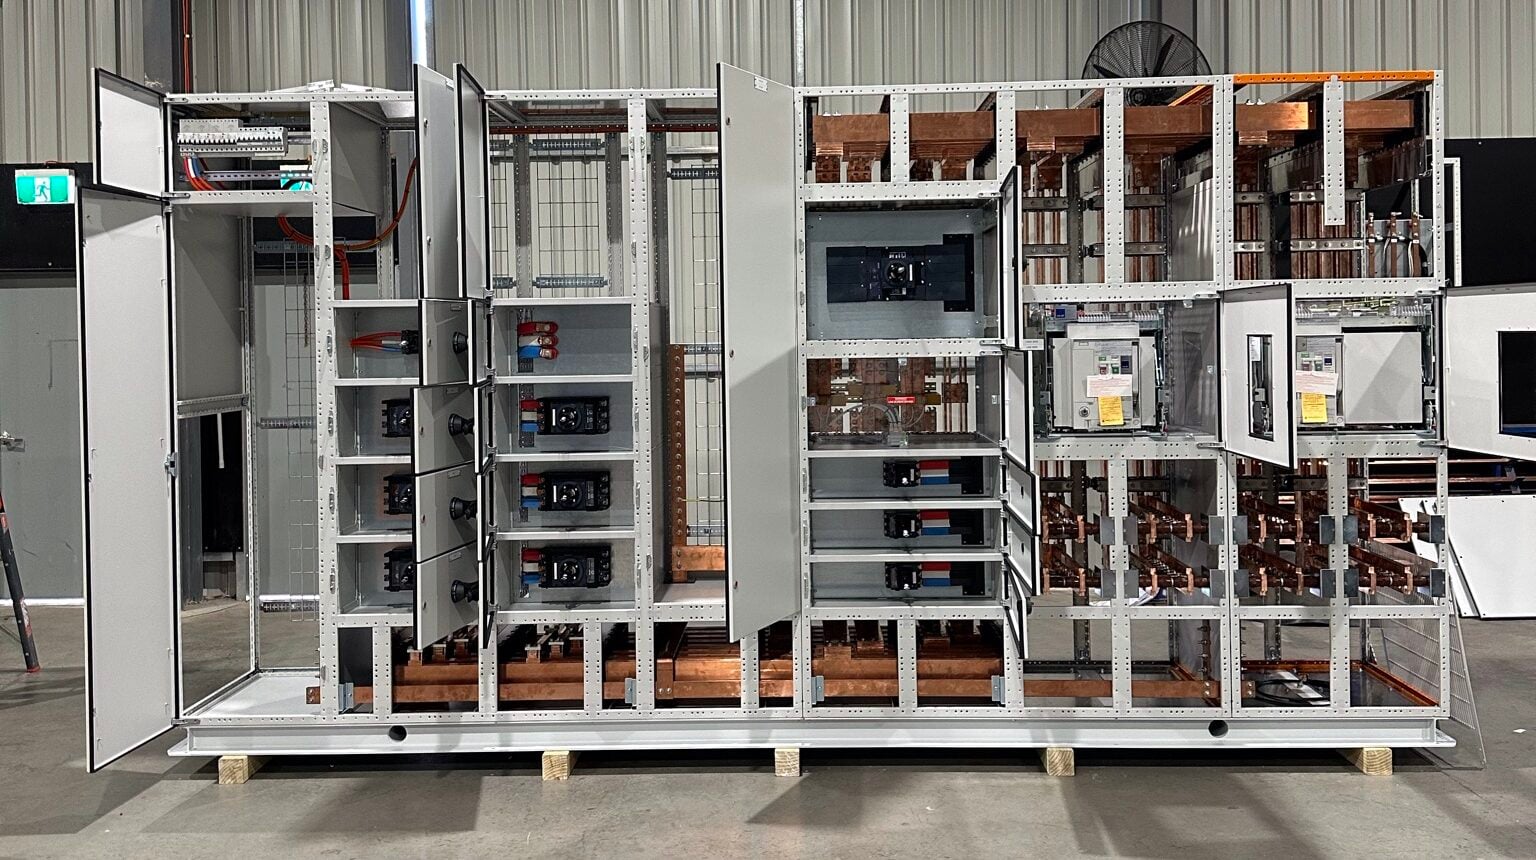
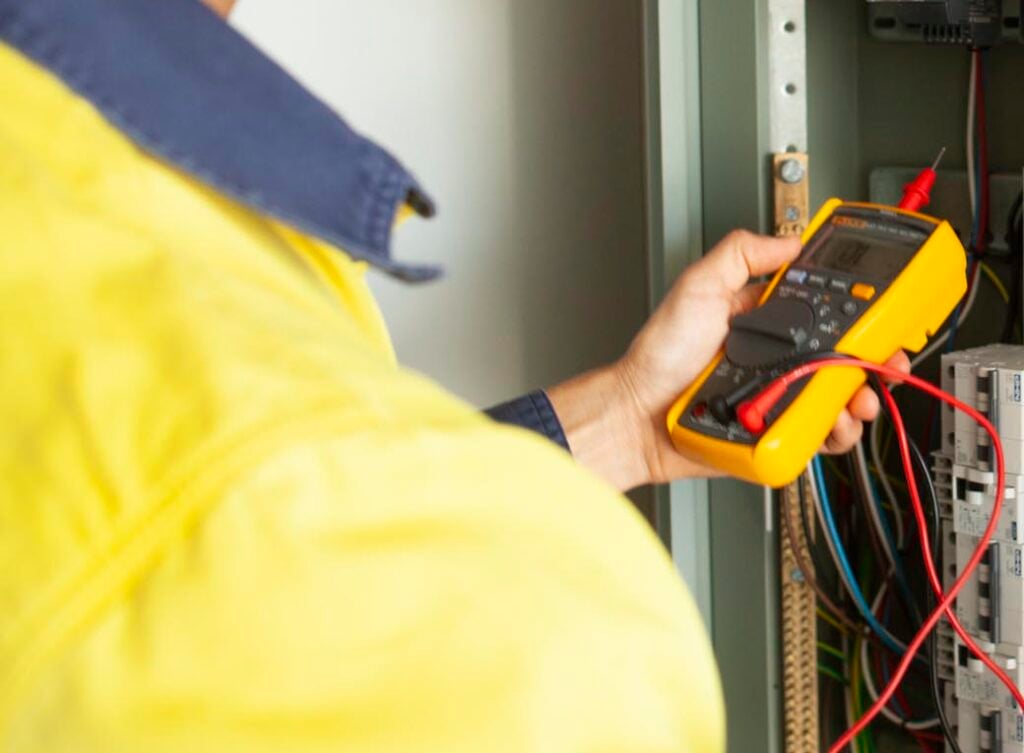
Designed, built and tested in our purpose-built facility.
I2R Switchboard Solutions For All Applications
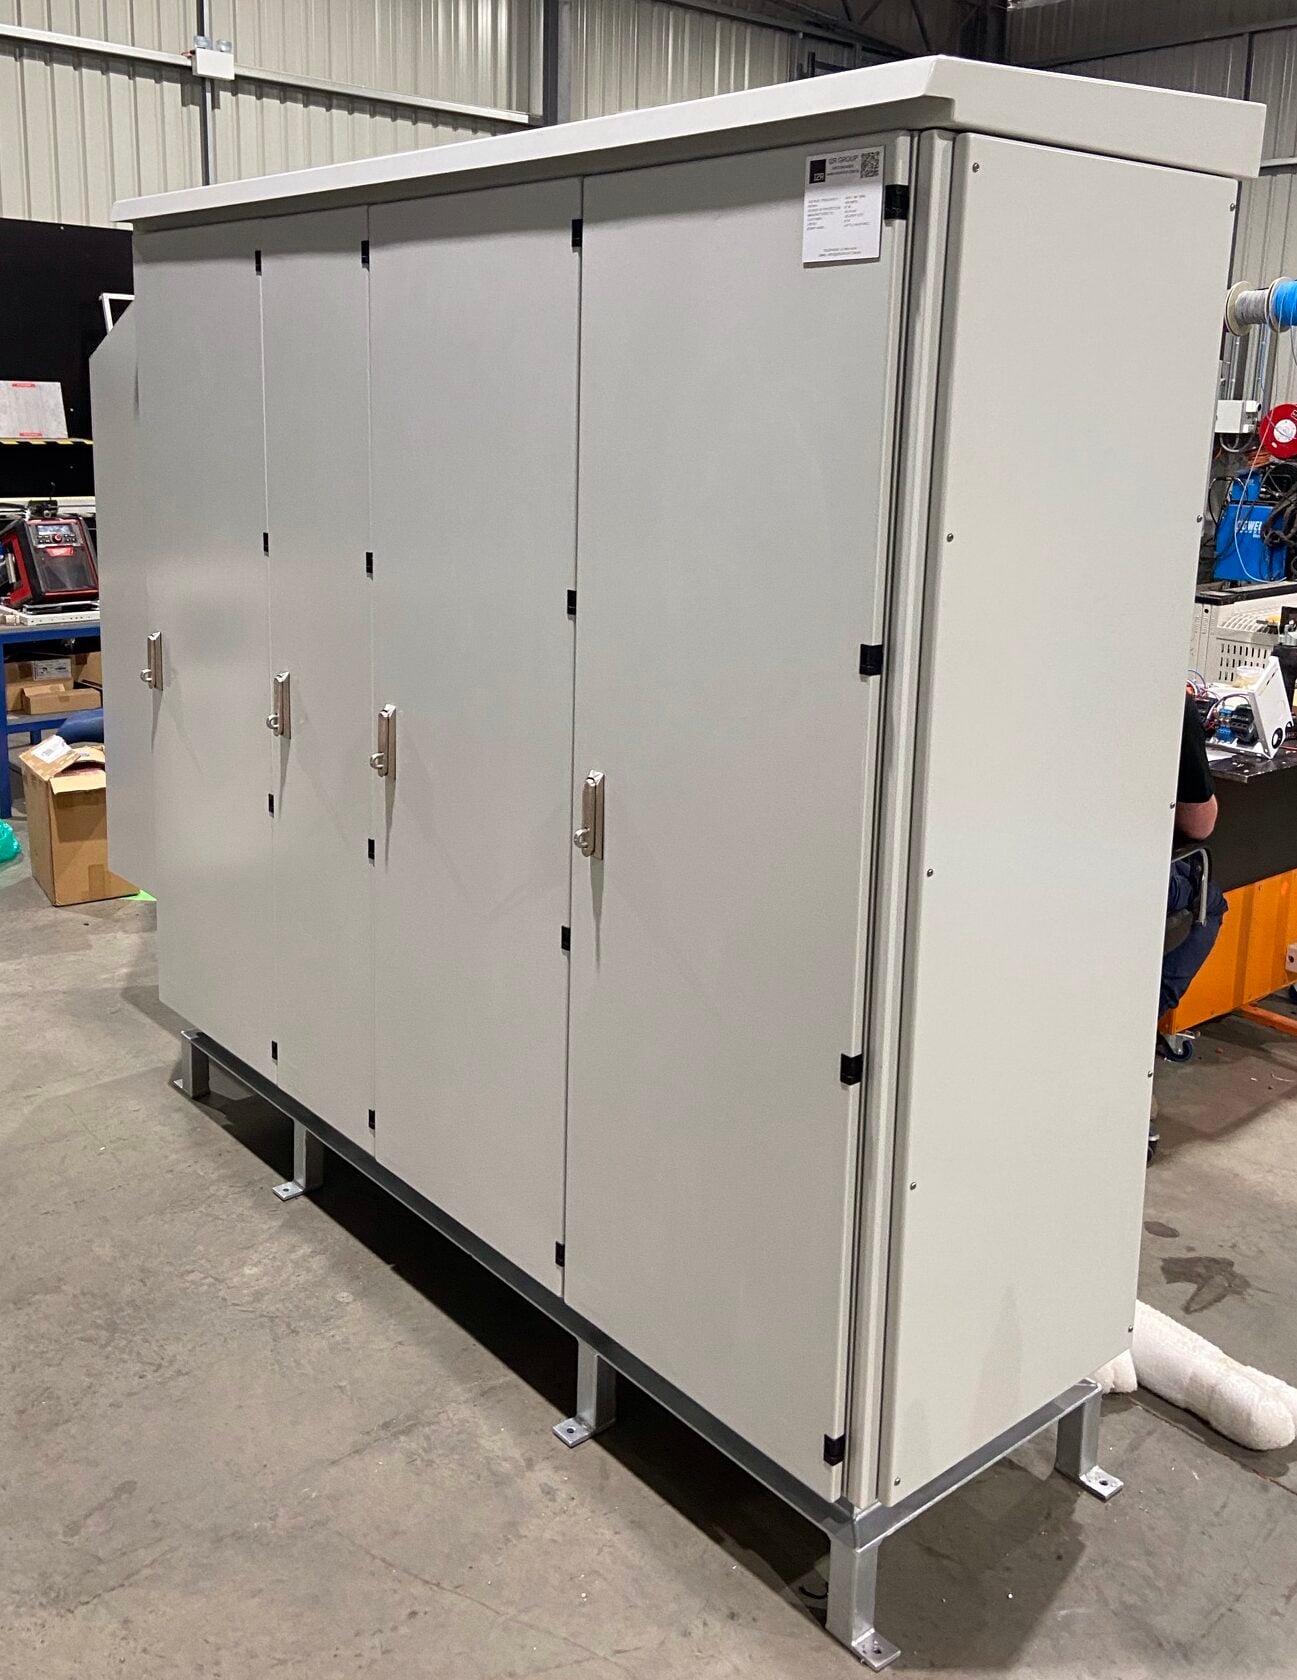
From a single distribution board to a complete containerised power and control solution, manufactured to Australian Standards under our quality system and delivered anywhere in Australia.
We control design, procurement, fabrication, wiring, testing and documentation in house.
We can deliver a board as a supply-only item or as part of a complete turnkey control system with PLC and SCADA programming, installation and commissioning.
Single point of accountability.Design, manufacture, software and commissioning sit under one contract and one warranty. There is no interface between switchboard supplier and integrator for you to manage.
02
Control of lead time.Your board is not queued behind a third-party board shop. Programme risk stays with a team you can call, in a facility you can visit.
03
Automation-literate boards.Boards are designed by the engineers who write the PLC and SCADA code, so I/O, drives, networking and safety are engineered together rather than reconciled on site.
04
Factory acceptance testing.Factory assembly and testing compresses site time and shutdown exposure, and lets you witness the board working before it leaves Griffith.
What we build
Switchboards and panels
Main switchboards (MSB) and main distribution boards (MDB)
Motor control centres (MCC), including bayable and withdrawable arrangements
Modular power distribution and sub-distribution boards
Variable speed drive and soft starter panels
PLC, control and instrumentation panels
Power factor correction and power quality panels, including static var generators
Load shedding and generator changeover / ATS boards
Field marshalling, isolation and local control stations
Stainless steel and IP-rated enclosures for washdown and corrosive environments
Seven stages, all performed by I2R people. Drawings, code, copper and commissioning never leave the business.
01
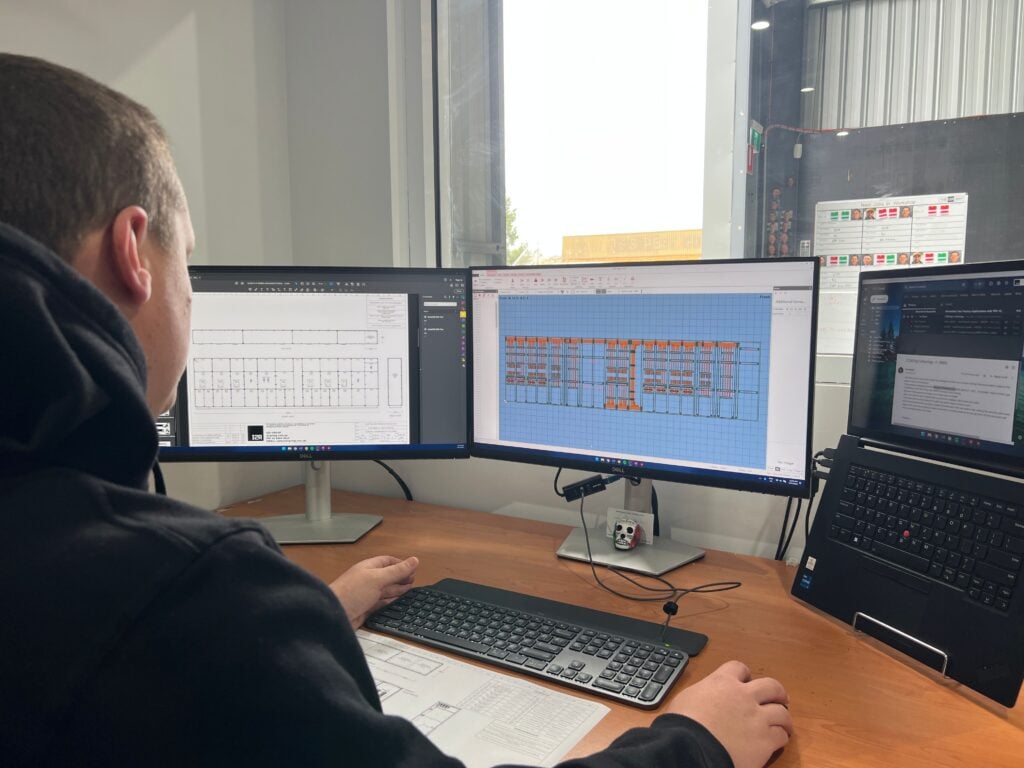
Scope and electrical design
Load schedules, single-line diagrams, protection and discrimination, form of separation and enclosure selection, reviewed with your engineers before manufacture.
02
Drafting and approval
Schematic, general arrangement and termination drawings produced in house and issued for approval. Design changes do not sit in a third-party queue.
03
Procurement
Switchgear, drives and enclosures sourced through our supply agreements with major manufacturers, with long-lead items ordered at design freeze.
04
Manufacture and wiring
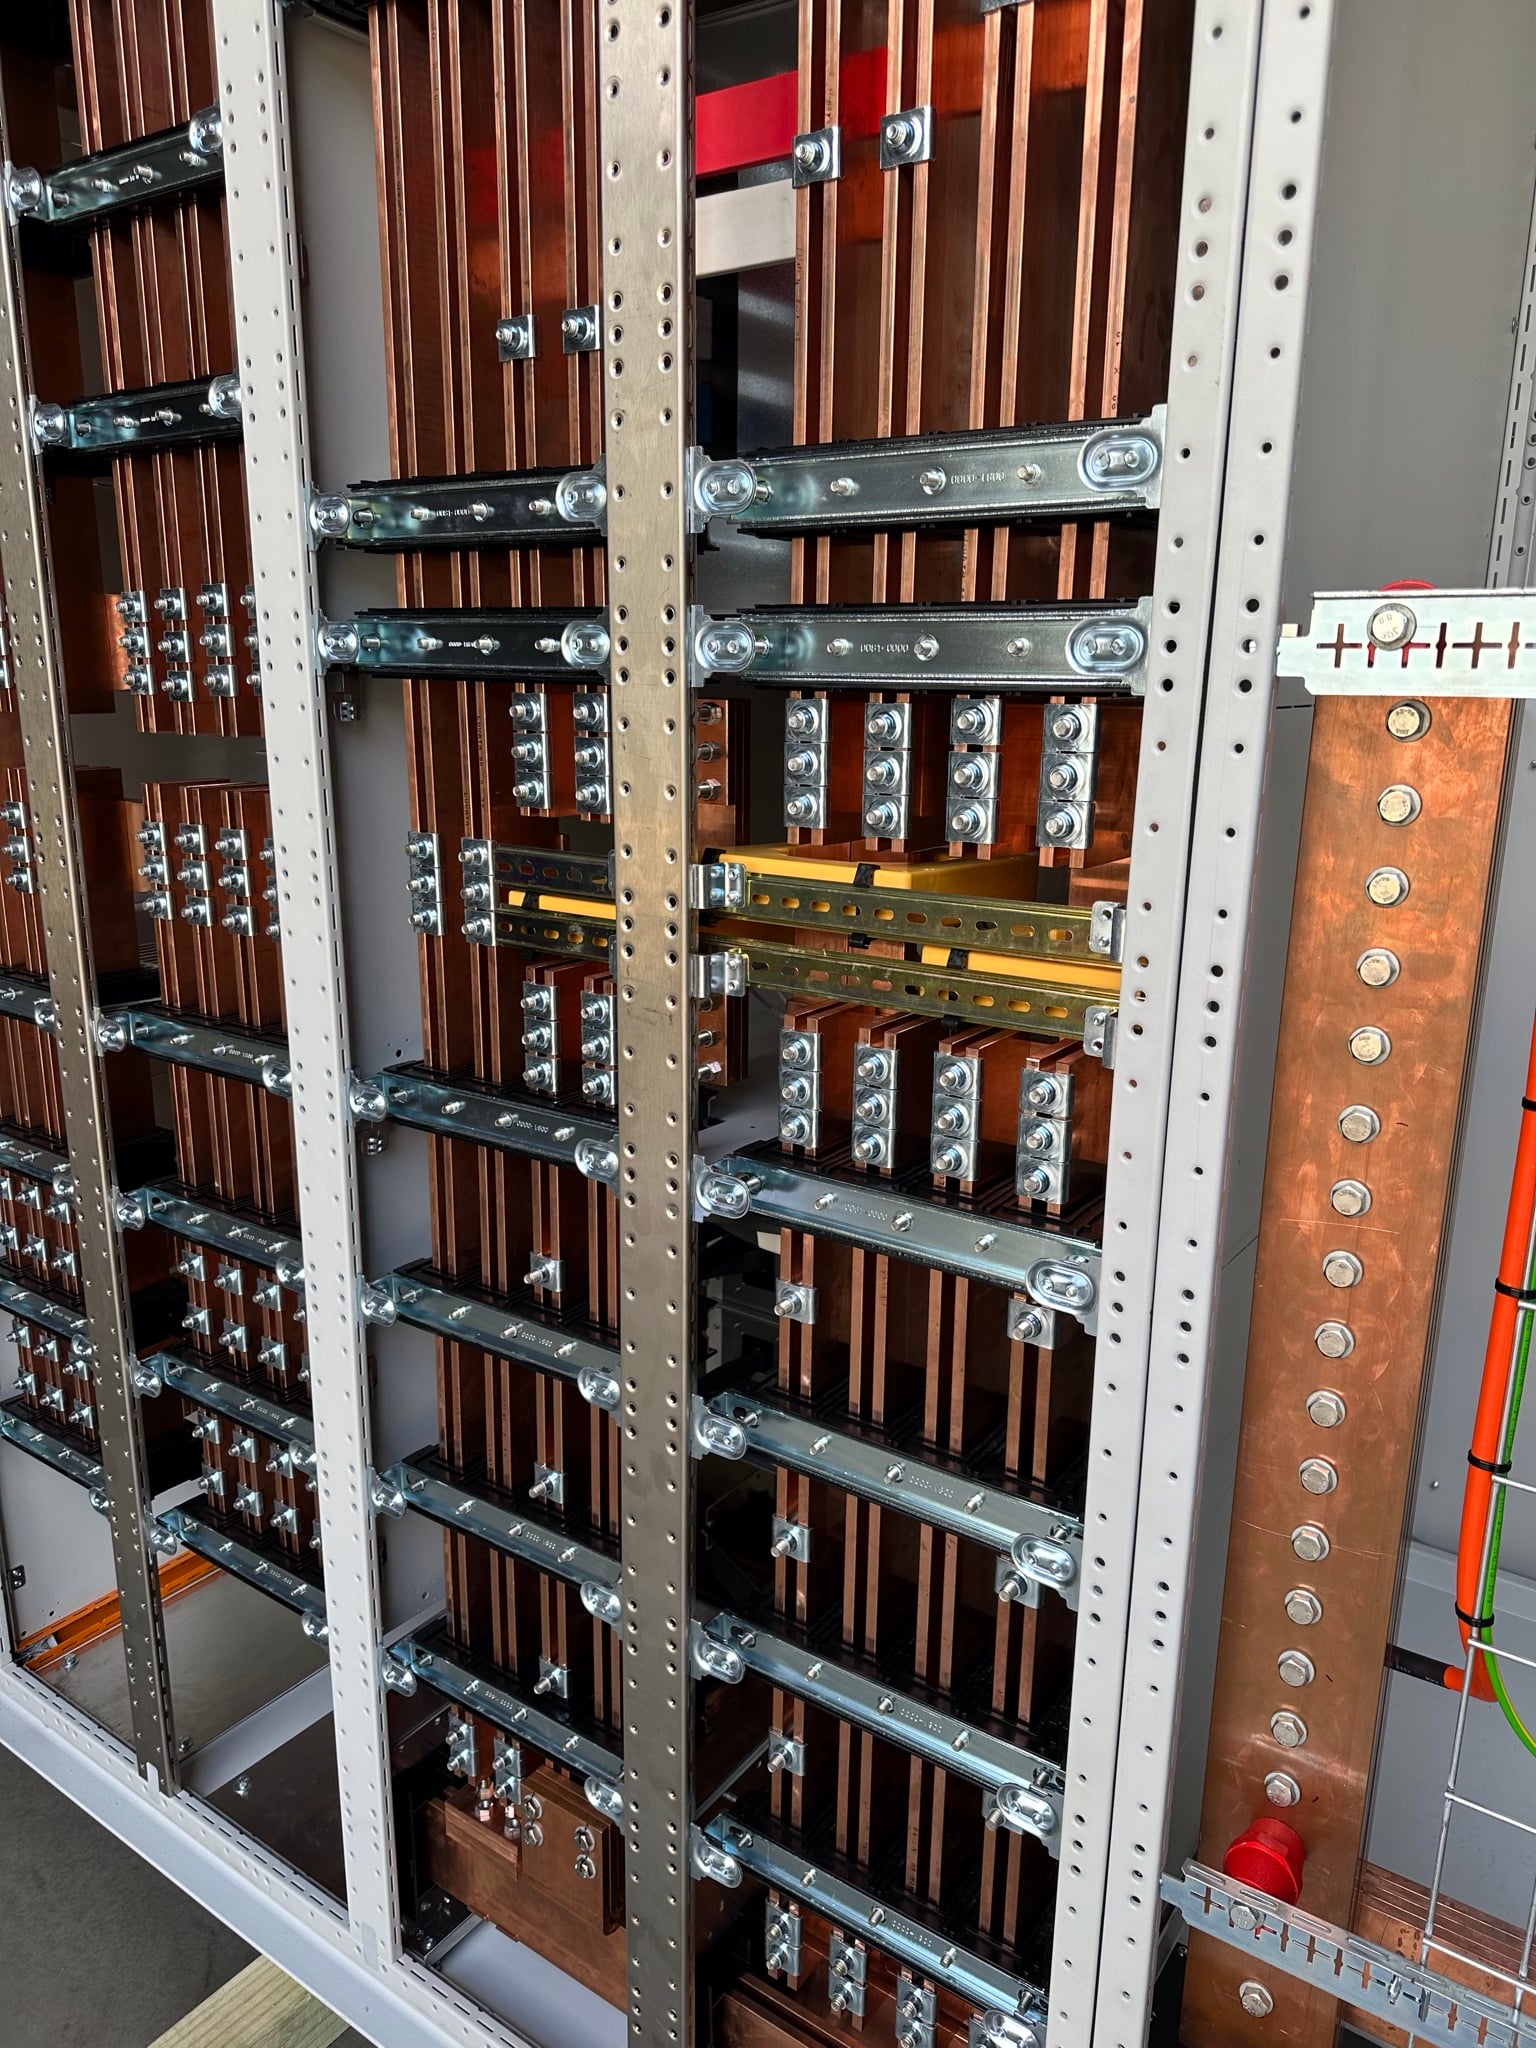
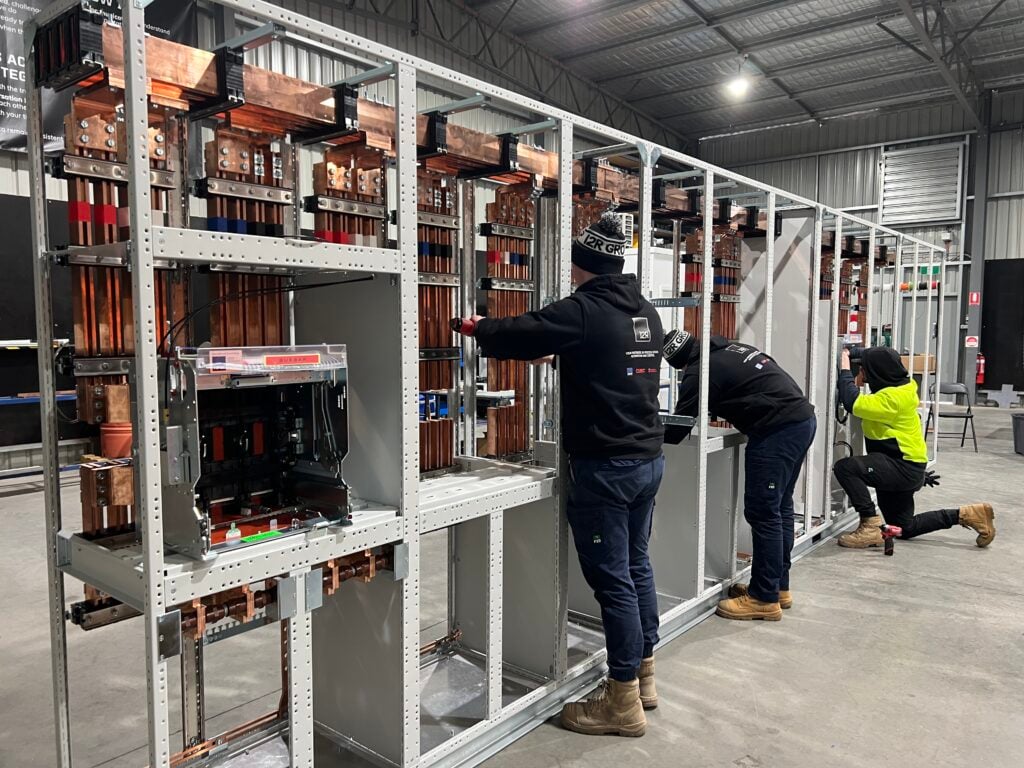
Fabrication, busbar assembly, equipment mounting, wiring and labelling in our Griffith facility under a documented quality system.
05
Test and inspection
Routine testing and inspection before despatch, with customer factory acceptance testing available. Test records issued with the board.
06
Delivery and commissioning
Transport, placement, site connection, PLC and SCADA integration, commissioning and operator handover by our own field teams.
07
Support and asset care
Ongoing service and maintenance including thermal imaging, sensor calibration, spares support and preventative maintenance programmes across the life of the installation.
Quality and standards
Manufactured to AS/NZS 61439 and installed to AS/NZS 3000. Safety, quality and sustainability practices follow ISO-aligned systems, and we are a Cubic accredited modular switchboard builder.
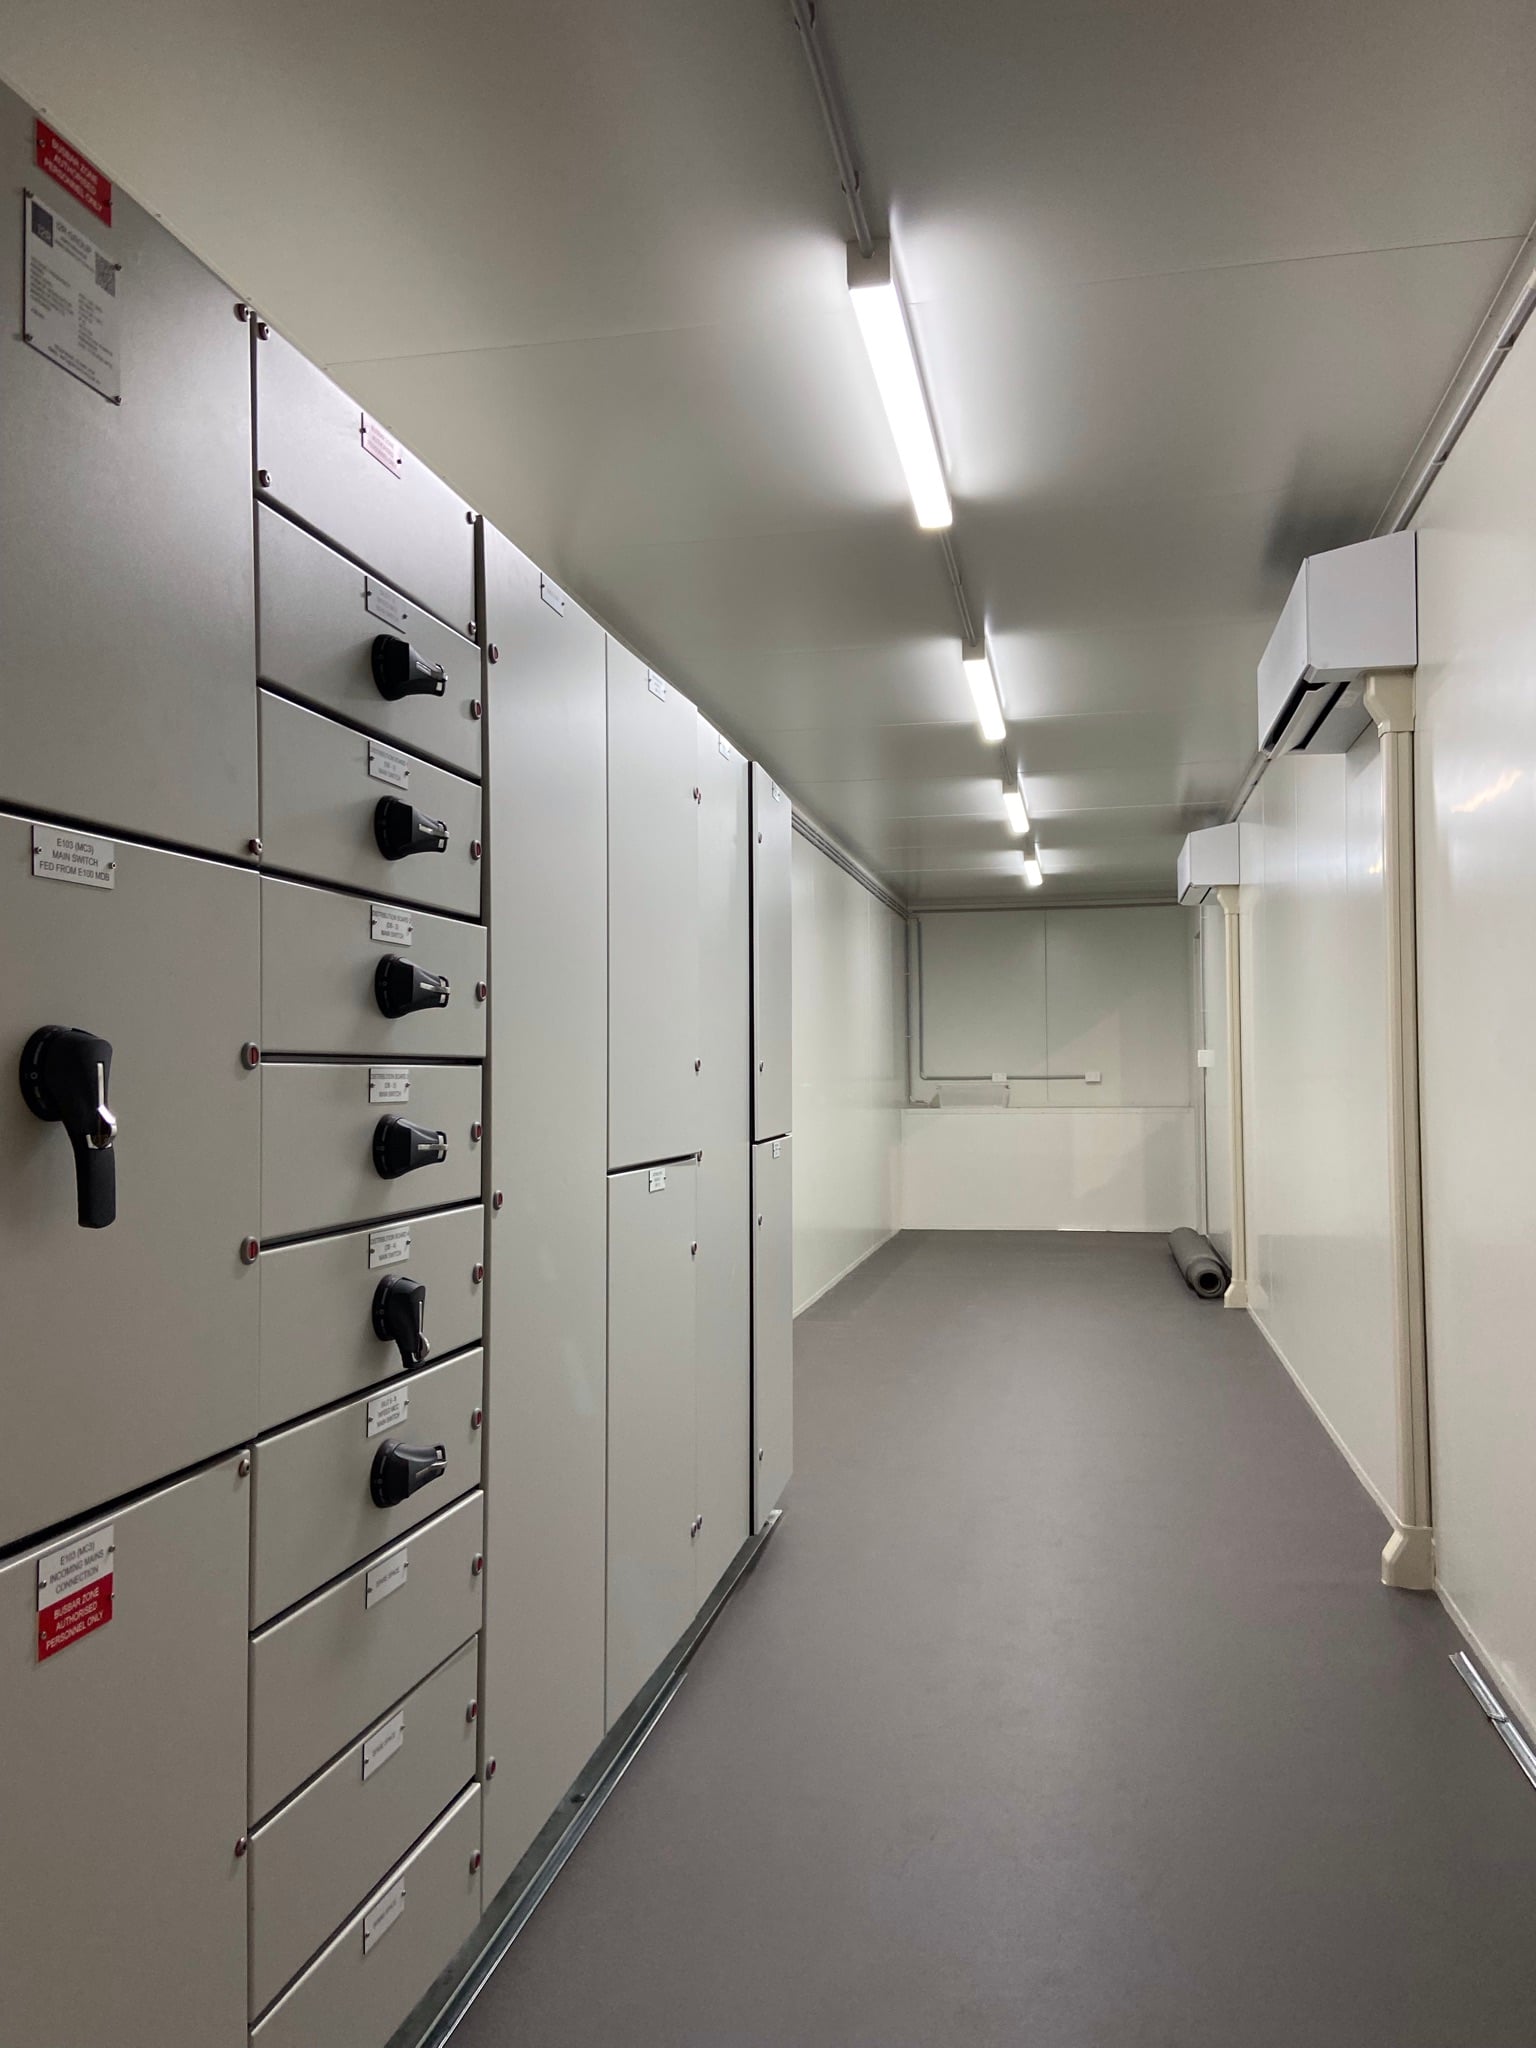
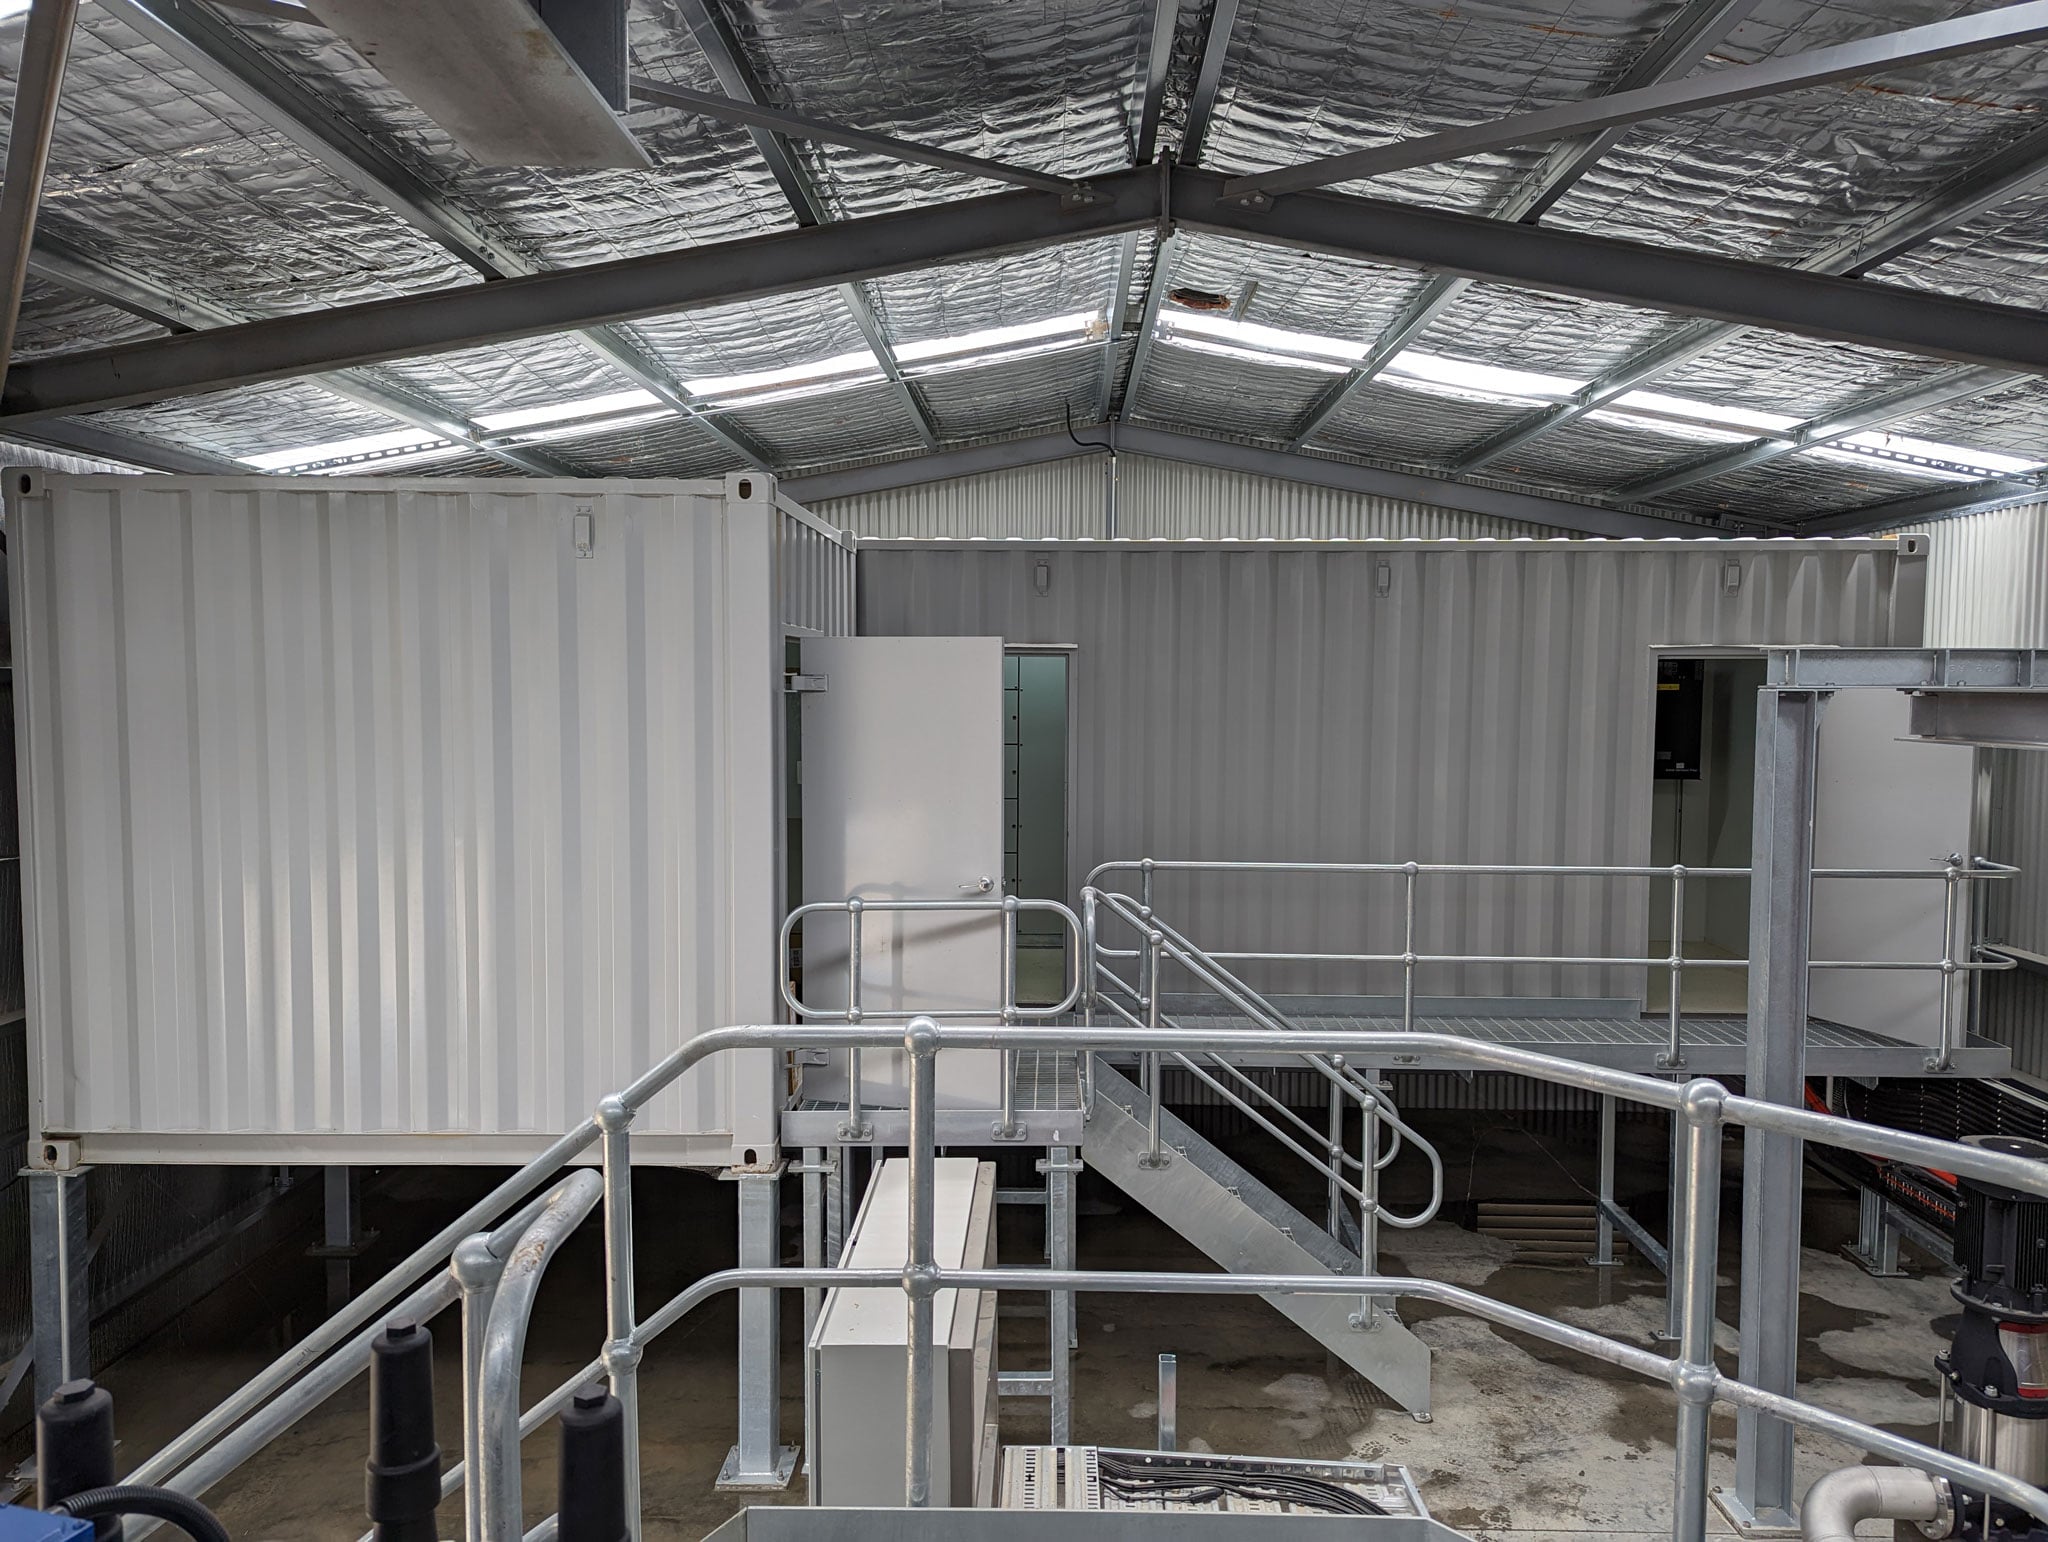
A remote plant processing facility could not access mains power at an efficient cost. I2R worked with the client’s project management team to design an off-grid power and distribution system, then designed and manufactured the prefabricated switchrooms and switchboards to run it.
Aim
Provide a reliable off-grid supply capable of running up to two generators at once, with provision for a third generator as backup, so the plant maintains a 100% operation rate through its nine-month annual processing program.
I2R solution
I2R designed and manufactured three switchboards for Stages 1 and 2 of a five-year, four-stage project:
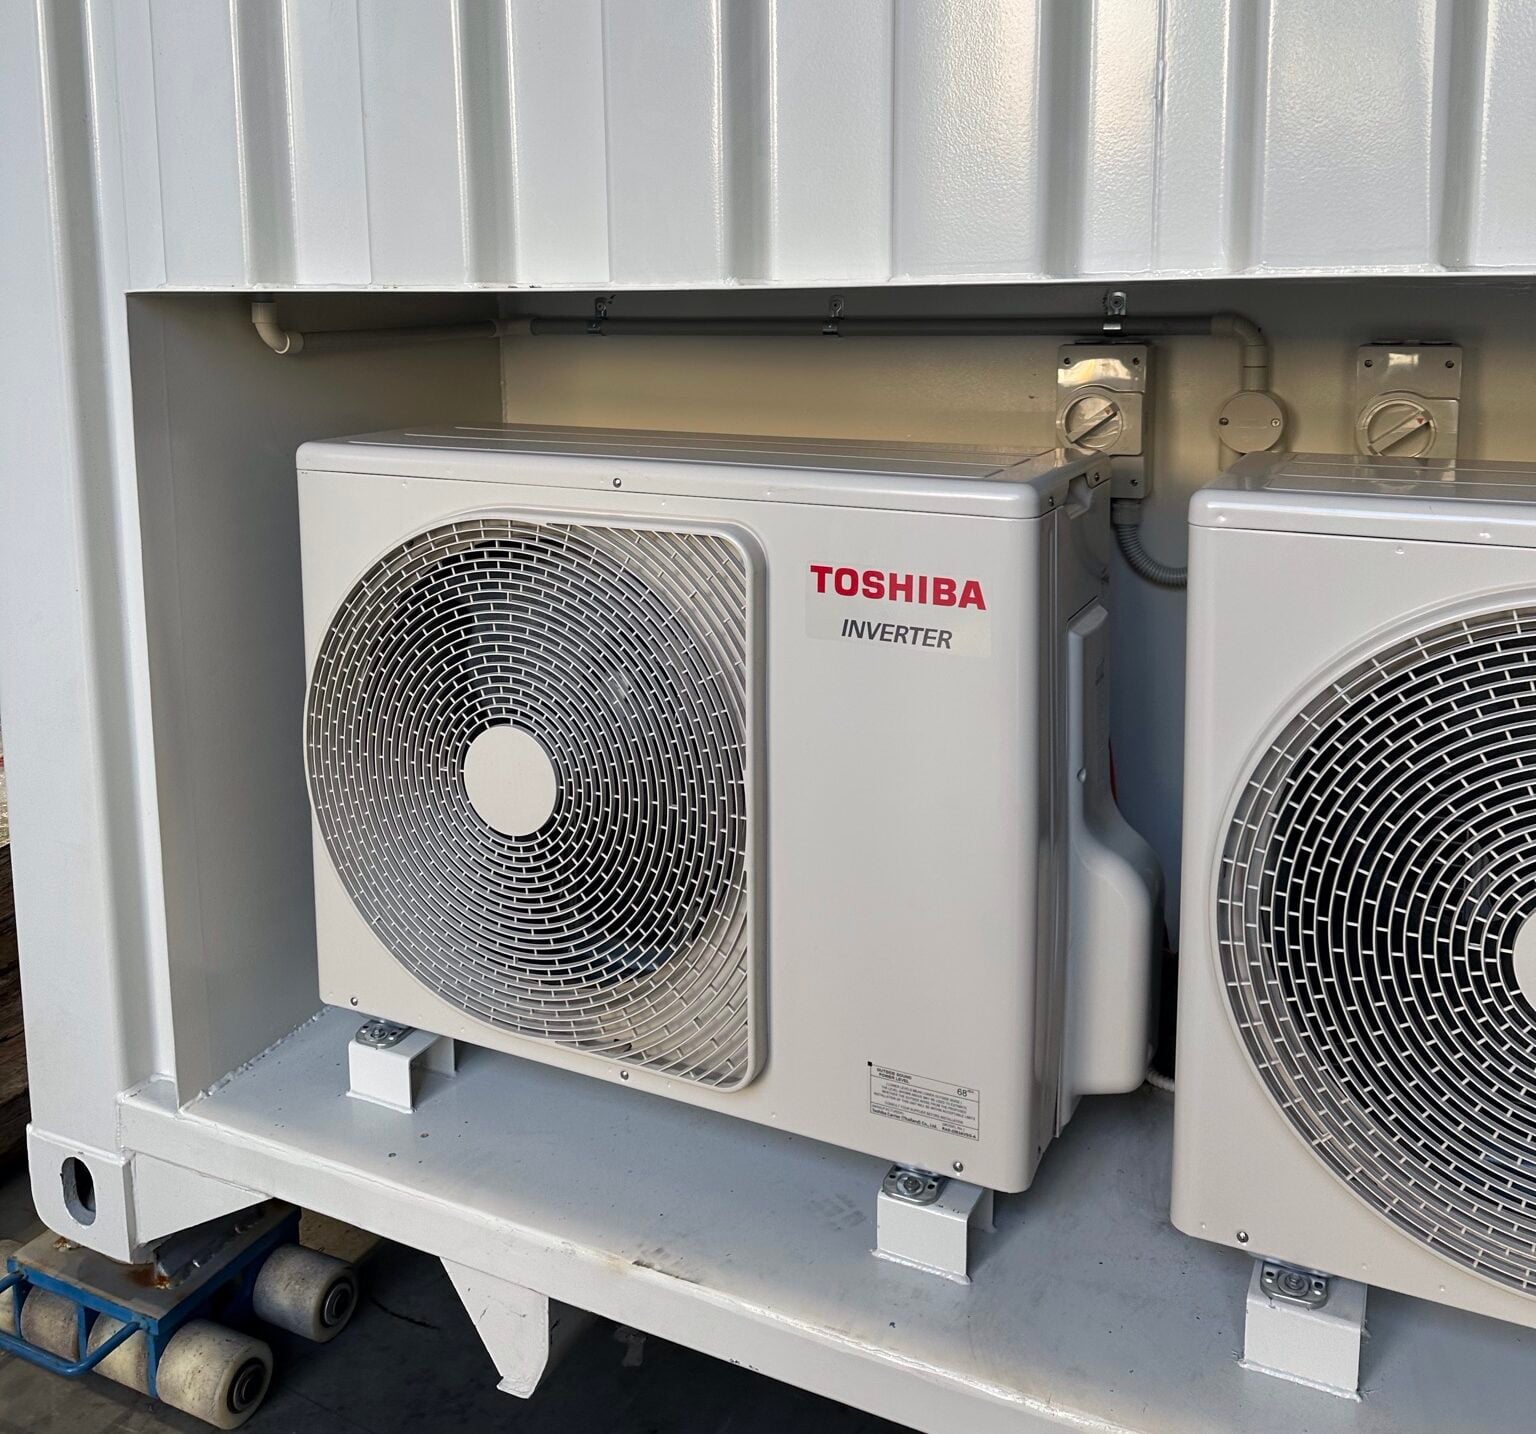
A 40ft / 12 metre prefabricated switchroom housing a 2000A main switchboard, powered by up to three generators and one solar system, and supplying four separate switchrooms over the life of the project.
A 1200A main distribution board and switchroom to power the OEM MCC equipment.
An 800A switchboard designed to power the OEM MCC equipment for Stage 2.
I2R is collaborating closely with the electrical team on site to ensure optimal delivery and installation, leveraging I2R’s manufacturing and delivery services.
Outcome
Continuous operation of the plant’s nine-month processing program each year, eliminating downtime and achieving optimal efficiency and reliability. The customer has realised a significant reduction in capital expenditure by removing the requirement for mains power infrastructure.
Capability
Off-grid power design, 2000A switchboard manufacture and 40ft prefabricated switchroom build, tested in Griffith and delivered to a remote site as a complete, staged power solution.
Looking for assistance with your next switchboard project? Our team of skilled designers, fabricators, and installers are here to help you achieve your switchboard needs.
Get in touch with us today and one of our friendly and highly trained staff members with be in touch.